How to Choose the Right Box Erecting Machine

Time:2026-11-08 Author:Aria
0%

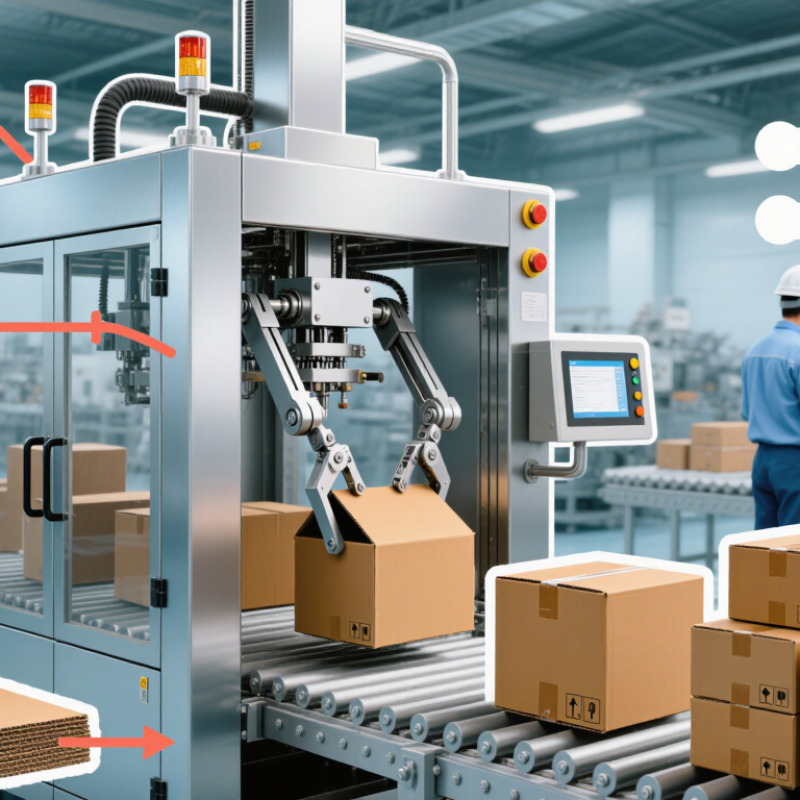
Choosing a Box Erecting Machine is not simply a matter of buying the fastest unit. It is a decision about how reliably your packaging line can turn flat corrugated blanks into square, usable cartons. PMMI’s 2024 State of the Industry report discusses automation, workforce pressures, and operational flexibility as important forces shaping packaging investment. Those pressures make equipment selection more practical than ever. A missed carton, a weak fold, or a slow changeover can interrupt the work around it.

The right choice depends on your actual cartons and production conditions. Compare the machine’s carton-size range with your smallest and largest boxes. Check its rated speed against the speed your team can consistently feed and downstream equipment can handle. Ask how it manages different board grades, blank quality, changeovers, and carton sealing. Grand View Research’s Packaging Machinery Market analysis offers broader context on demand for packaging equipment, but market growth alone cannot tell you which machine fits your plant. Your own product mix matters more. A compact machine may suit a tight floor plan; a higher-output model may make sense where demand is steady. The trade-offs are real. Even an impressive specification sheet can hide a difficult setup or maintenance routine. Request a demonstration using your cartons, and ask operators to assess access, adjustments, and fault recovery. A little hesitation is useful here. The best machine is not always the most advanced one; it is the one your team can run reliably, maintain, and adapt as requirements change.
How to Choose the Right Box Erecting Machine

Define Carton Dimensions, Board Grades, and Required Cases per Minute

How to Choose the Right Box Erecting Machine

Define the cartons before comparing machine speeds. Record each box’s internal length, width, and depth, plus blank dimensions, flap lengths, and closure style. Check the smallest and largest sizes you actually run. A machine’s stated range may not cover every combination reliably. Small details matter.

Board grade affects how blanks feed and how corners hold shape. Note flute type, thickness, and supplier tolerances; a stiffer board may need different vacuum or folding settings. FEFCO’s 2022 European Database reports 50.2 billion square metres of corrugated board production in Europe. That scale reflects a wide range of board constructions, not one universal setup. Test with production blanks, including warped or dusty samples. Clean samples can flatter a machine.

Set the required cases per minute from real demand, not a peak-hour guess. Calculate average demand, then include short surges, replenishment delays, and downstream stoppages. PMMI’s 2023 State of the Industry report recorded 9.3% growth in U.S. packaging machinery shipments in 2022, a reminder that automation capacity is an active investment decision. Treat nameplate speed as a starting point. Run a timed trial with your carton sizes and board grades, and check changeover time. I would allow operating headroom, but there is no single percentage that fits every line.

Compare Semi-Automatic and Automatic Models Rated at 10–30 Cases per Minute

Choosing between semi-automatic and automatic box erectors rated at 10–30 cases per minute starts with the work around the machine. A semi-automatic unit suits lower-volume lines where an operator loads blanks or completes part of the setup. It can be easier to justify when demand changes often. An automatic model feeds, squares, and erects cases with less routine handling. That can help steady output, but requires space, maintenance, and reliable blank supply.

Rated speed is a ceiling, not a promise. Case dimensions, board quality, changeovers, and replenishment interruptions all affect real production. PMMI’s 2024 State of the Industry report estimated U.S. packaging machinery shipments at $10.9 billion in 2023. This shows a substantial equipment market, but does not predict any one line’s performance. Ask suppliers to demonstrate your actual case sizes at several speeds. Track good cases per minute over a full shift, not just during a brief test. I would leave some room for uncertainty; carton blanks rarely behave perfectly every day.

Tip: Before choosing, record hourly demand, changeover frequency, available floor space, and operator time. Compare total usable output, not headline speed. A short trial with your own corrugated blanks can reveal jams, awkward loading, or setup delays.

Assess Magazine Capacity, Changeover Time, and Line Integration

A box erecting machine’s magazine should match actual carton use, not just the longest run on the schedule. Estimate blanks consumed per minute, then calculate how often an operator must refill the magazine. Watch a full shift if possible; short trials can hide awkward refill timing. A larger magazine may reduce stops, but it also takes floor space and can make blank loading less comfortable. Check that cartons feed cleanly when the stack is nearly full and nearly empty.

Changeover time depends on more than the machine’s adjustment settings. Measure the time from the last acceptable carton in one size to the first acceptable carton in the next. Include guide adjustments, blank loading, test cycles, and any minor corrections. That number matters. Ask operators to perform the changeover, then note where they pause or reach for tools. A quick change on paper may feel fiddly on the floor, and that difference is worth investigating.

Line integration deserves the same attention. Compare the erector’s steady output with the pace of the sealer and downstream conveyor, not just their advertised maximum rates. Confirm carton dimensions, blank orientation, transfer height, and available accumulation space. Test both the smallest and largest cartons planned for production. A sensor or conveyor gap that works with one size may cause occasional misfeeds with another. Leave room for maintenance access, too; a tightly fitted layout can look efficient until a jam needs clearing.

Verify Box-Closing Methods Against ASTM D1974

ASTM D1974 describes practices for closing, sealing, and reinforcing fiberboard boxes. It can help you compare a machine’s closure method with your packaging requirements. It is not a machine-performance certification or a guarantee that every box will survive distribution. Check the current standard and confirm which procedures apply to your box style.

Run trials using the actual carton dimensions, board grade, and closure materials. Watch how the machine folds the flaps and applies tape, adhesive, or other specified closures. Look for lifted edges, gaps, uneven tape overlap, and crushed corners. A neat seam can still hide weak compression. Small details matter. Record settings, line speed, and any changes, then inspect boxes after normal handling and stacking. If the machine will process several carton sizes, test each representative format rather than relying on one ideal sample.

ASTM D1974 provides a useful reference, but real results depend on the box, contents, and operating conditions. Humidity and conveyor transitions can change how a closure performs. That part is easy to underestimate. Compare observed results with your shipping needs, and involve packaging or quality staff when interpreting the standard. A brief trial may reveal an awkward flap or inconsistent seal; it may also leave questions worth checking before purchase.

How to Choose the Right Box Erecting Machine - Verify Box-Closing Methods Against ASTM D1974

ASTM D1974 is a standard practice covering methods for closing, sealing, and reinforcing fiberboard boxes. Use the current edition alongside your packaging specification and product testing; the standard does not certify a machine or select one universal closure method.

Closing method Typical machine setup Often suitable for Selection considerations What to verify during evaluation ASTM D1974 connection
Pressure-sensitive tape Case erector with a tape head that applies tape across the bottom flaps; a separate sealer may close the top. Many routine shipping applications where quick application and straightforward changeovers are useful. Tape width and backing, carton surface, application pressure, flap alignment, and storage or shipment conditions can affect adhesion. Confirm consistent tape placement and contact, secure adhesion at the flap edges, and that the chosen tape and carton perform in the intended distribution environment. Closing / sealing method
Water-activated tape Case erector fitted with a tape dispenser that wets and applies gummed tape to the box flaps. Applications seeking a bonded tape closure; suitability depends on the carton, tape construction, and operating conditions. Water application, tape wet-out, compression, and adequate bonding time need to be controlled. Check tape wetting and placement, bond development, adhesion to the actual corrugated surface, and performance after conditioning appropriate to the shipment. Closing / sealing method
Hot-melt adhesive Case erector with an adhesive applicator that applies hot-melt beads or patterns before the flaps are pressed together. Production lines where an automated adhesive application process fits the carton design and throughput requirements. Adhesive type, application pattern, temperature, open time, compression, and carton surface affect the resulting bond. Verify the specified adhesive and application pattern, flap contact, bond consistency, and safe operation at the required production rate. Closing / sealing method
Staples Case erector equipped with a stapling head to mechanically fasten carton flaps. Box designs and handling requirements for which a mechanical fastener is specified and permitted. Fastener size and placement must suit the board construction; consider product protection, worker safety, and handling requirements. Inspect staple placement, clinching or fastening quality, carton damage, and any product-contact or safety restrictions in the packaging specification. Closing method
Strapping reinforcement Typically added by a downstream strapping machine after the box has been erected and closed. Packages whose design or distribution requirements call for additional reinforcement or unitizing. Strap material, position, tension, and interaction with the box and contents should be specified; excessive tension may damage the package. Confirm strap location and tension are repeatable and that the completed package withstands the applicable handling and distribution tests. Reinforcing method
Folded-flap closure Case erector forms and folds the flaps; a separate sealing or fastening step may or may not be required by the package design. Carton styles designed to close by folding, where the box specification allows that construction. Flap geometry, board condition, contents, and retention during handling determine whether folding alone is appropriate. Check that flaps fold in the intended sequence, remain in position as designed, and meet the package specification under expected handling conditions. Closure method

Compare Total Cost of Ownership, Maintenance, and Operator Requirements

Compare box erecting machines by total cost of ownership, not purchase price alone. Include tooling, format-change parts, electricity, compressed air, labor, and expected downtime. Ask for the assumptions behind quoted output rates. A machine rated for high speed may run slower with your carton sizes or inconsistent board quality. Small details matter.

Maintenance affects both cost and production continuity. Check how often the machine needs cleaning, lubrication, adjustments, and replacement parts. Ask whether common wear items can be changed with standard tools, and how quickly critical spares can be supplied. A simple maintenance schedule is useful, but only if your team can follow it during busy shifts. Downtime estimates are rarely exact.

Operator requirements deserve equal attention. Observe a changeover, not just a demonstration at steady speed. Note how many controls the operator must monitor, whether jams are easy to clear, and how much training is needed. Clear instructions and accessible safety features can reduce errors and help new staff work confidently. If one skilled person must constantly adjust the machine, that labor cost belongs in the comparison. The cheapest option may still fit your operation, but verify it with a trial using your actual cartons and shift conditions.

FAQS

What carton details should I record before choosing a machine?

Record internal length, width, and depth, plus blank size, flap length, and closure style. Check the smallest and largest cartons you actually run. Small details matter.

How does board grade affect machine performance?

Flute type, thickness, and supplier tolerances can change how blanks feed and corners hold shape. Test with real production blanks, including dusty or slightly warped ones. Clean samples can flatter a machine.

How should I estimate the required speed?

Calculate average demand and account for short surges, replenishment delays, and downstream stoppages. Treat the stated speed as a starting point, then time a trial with your cartons. A peak-hour guess may mislead.

How can I tell whether magazine capacity is sufficient?

Estimate blanks used per minute and how often an operator must refill the magazine. Watch a full shift if possible. A larger magazine may reduce stops, but it needs space and comfortable loading access.

What should I include when measuring changeover time?

Measure from the last acceptable carton in one size to the first acceptable carton in the next. Include guide adjustments, blank loading, test cycles, and small corrections. Paper estimates can feel too neat.

How do I check whether the machine will fit into my production line?

Compare its steady output with the sealer and downstream conveyor. Check carton dimensions, blank orientation, transfer height, and accumulation space. Test both size extremes.

What should I inspect during a box-closing trial?

Use the actual carton, board grade, and closure materials. Look for lifted edges, gaps, uneven tape overlap, and crushed corners. A neat seam may still hide weak compression.

Are standard closure practices enough to confirm box performance?

No. Reference the applicable closure procedures, then inspect boxes after normal handling and stacking. Humidity and conveyor transitions can affect results. I would still check with packaging or quality staff.

Conclusion

Choosing the right Box Erecting Machine starts with understanding the cartons your operation handles. Confirm box dimensions, board grades, and the number of cases required per minute, then compare semi-automatic and automatic models rated for roughly 10–30 cases per minute. The best fit is not always the fastest machine; it should reliably meet demand while accommodating the materials and carton sizes used in daily production.

Also consider magazine capacity, changeover time, and how the machine will connect with upstream and downstream equipment. Check that its box-closing method aligns with the relevant requirements of ASTM D1974 and suits your packaging process. Finally, compare total cost of ownership, including purchase, maintenance, parts, and operator time. A machine that is straightforward to adjust and maintain can help reduce interruptions and support consistent production over time.
Aria

Aria

Aria is a dedicated marketing professional with a deep passion for innovative strategies and a keen understanding of our company's product offerings. With a wealth of experience in the industry, Aria excels at crafting engaging content that highlights the unique features and benefits of our......